Automatic Pipe & Flange Welding Machine
Automated Circumferential Welding System for Pipes, Flanges & Fittings
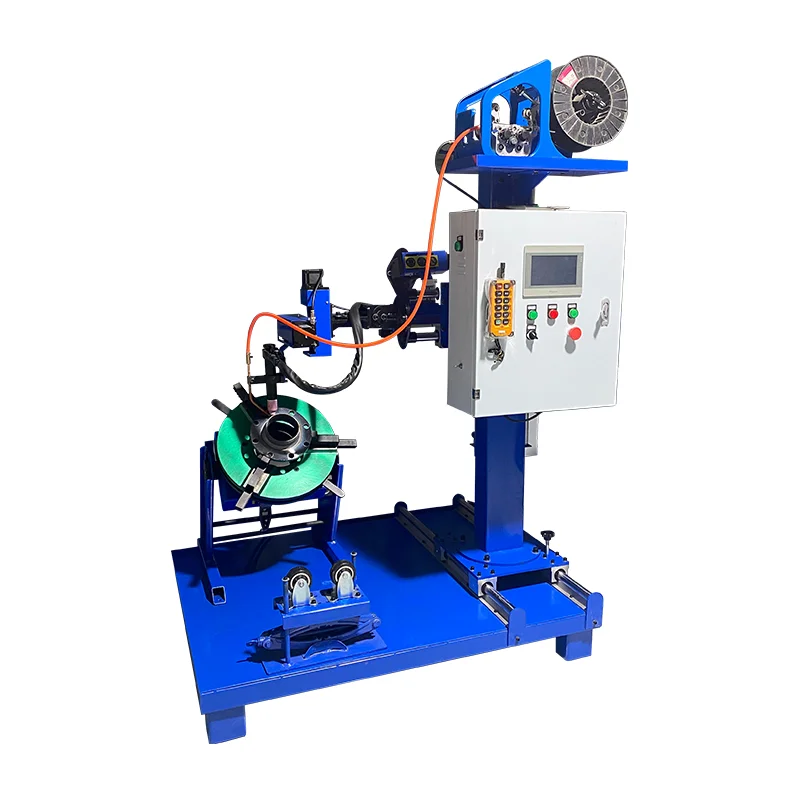
The Automatic Pipe & Flange Welding Machine is designed for automated circumferential welding of pipes, flanges, elbows and other pipe fittings.
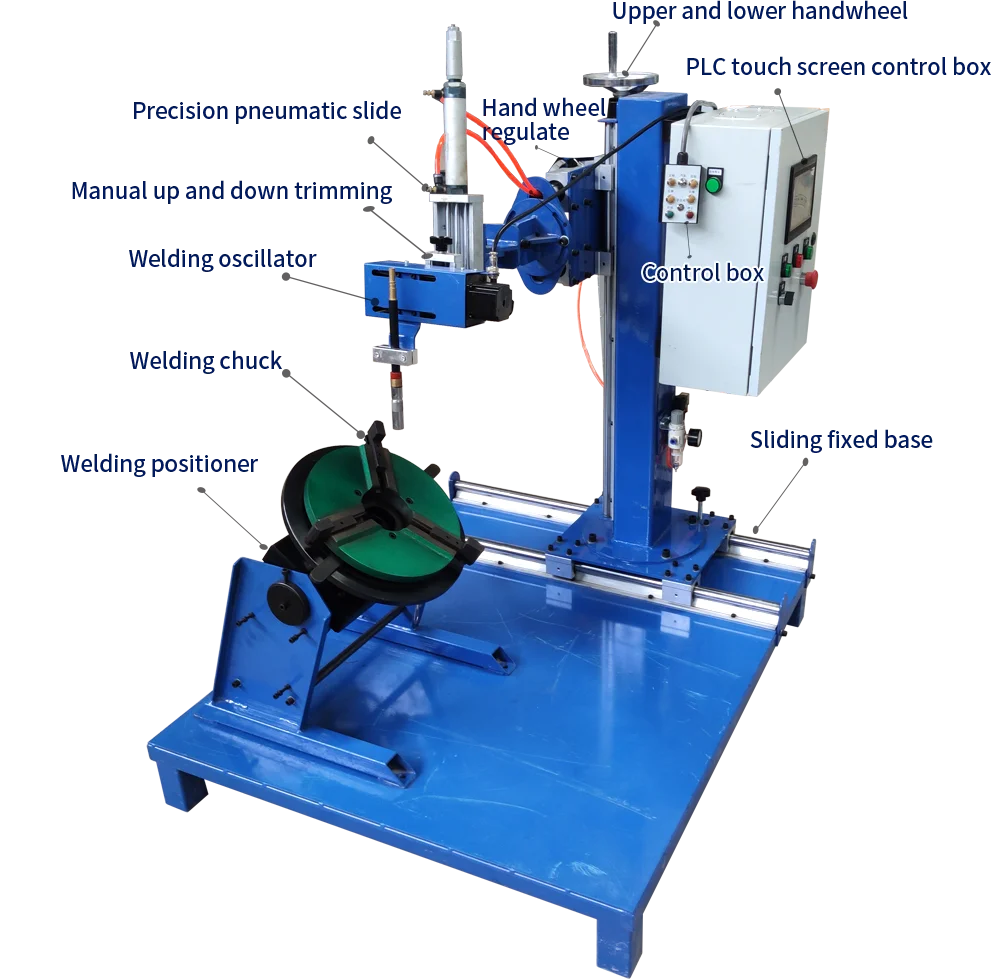
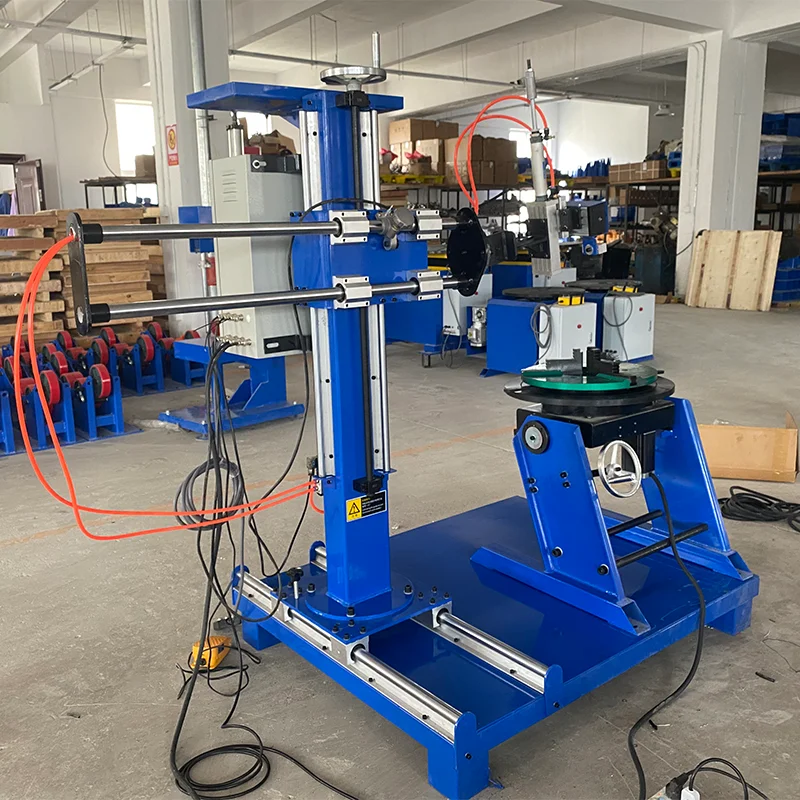
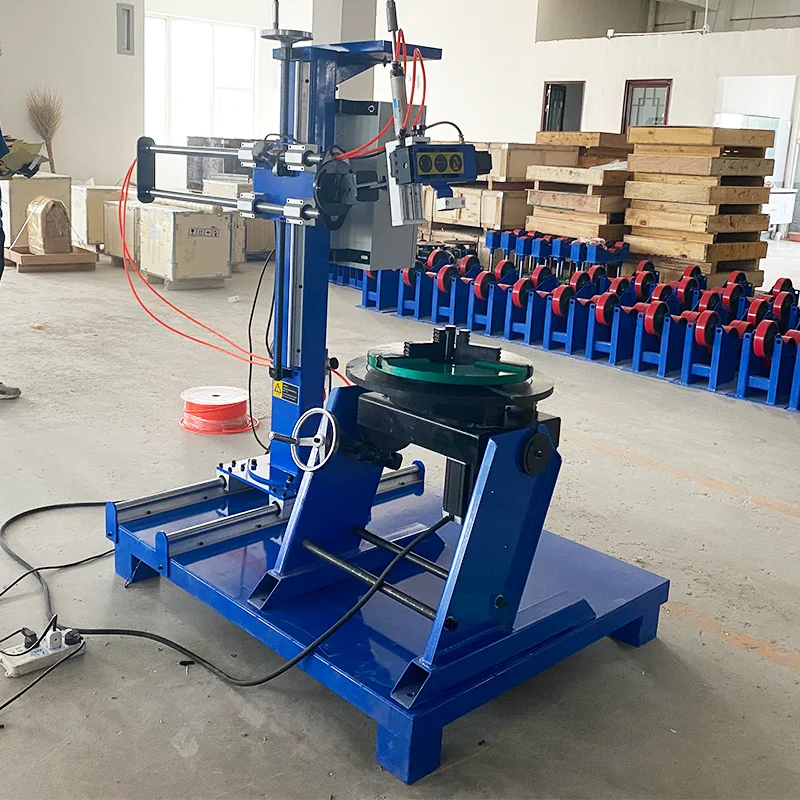
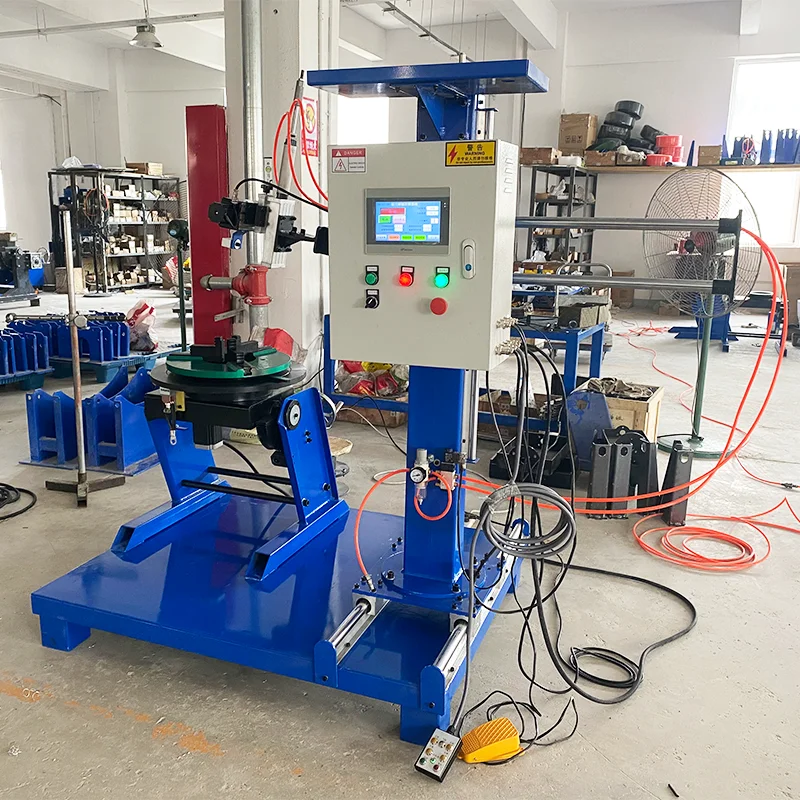
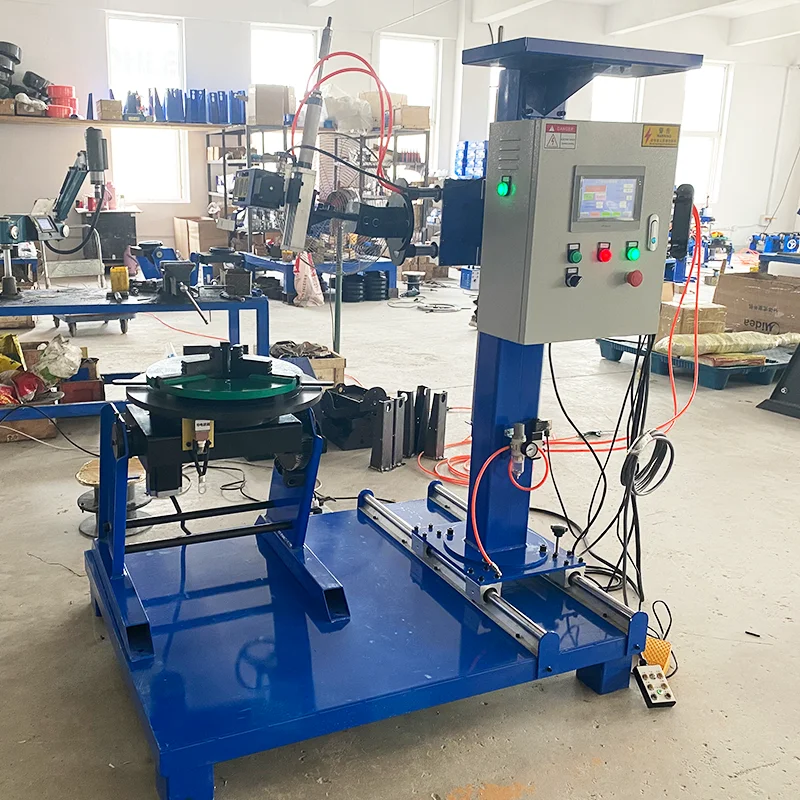
Its cantilever-type structure combines a welding positioner, workpiece chuck, movable welding unit, torch adjustment system and PLC control into an integrated welding workstation.
The system is particularly suitable for long pipe sections with multiple circumferential weld joints, allowing the welding unit to move between welding positions while reducing the need to repeatedly move and reposition the complete pipe assembly.
Applications: Pipe-to-Pipe / Pipe-to-Flange / Pipe-to-Elbow
Clamping Range: 20–500 mm
Positioner Horizontal Load: 300 kg
Positioner Vertical Load: 150 kg
Tilting Range: 0–90°
Welding Processes: Argon Arc / CO₂ Shielded / Submerged Arc
One System for Pipe, Flange & Fitting Welding
- Pipe-to-Pipe Welding
Automated circumferential welding for pipe sections and pipeline fabrication. - Pipe-to-Flange Welding
Designed for consistent circumferential welding between pipes and flanges. - Pipe-to-Elbow Welding
Suitable for automated welding of pipe-to-elbow connections. - Other Pipe Fittings
The system can also be used for welding applications involving tees and other pipe fittings, depending on workpiece dimensions and machine configuration.
Key Features
Automated Circumferential Welding
The workpiece is held and rotated by the welding positioner while the welding torch remains at the controlled welding location, providing a practical solution for automated circumferential welding.
Cantilever-Type Welding Structure
The cantilever design allows the welding unit to be repositioned along the workpiece, making the system suitable for long pipe sections containing multiple weld joints.
Reduced Workpiece Handling
Multiple weld joints can be processed without frequently moving the complete pipe or fitting assembly, which is one of the principal advantages described for this machine.
PLC Touchscreen Control
The system is equipped with a PLC touchscreen control box for centralized operation of the welding equipment.
Adjustable Welding Torch
The torch position can be adjusted according to workpiece dimensions, including vertical and front/rear positioning.
Welding Oscillator
A welding oscillator is available for applications requiring controlled torch oscillation. The ZDH-300 specification lists an 80 mm oscillation stroke.
Multiple Welding Processes
Depending on configuration, the system supports:
- Argon arc welding
- CO₂-shielded welding
- Submerged arc welding
The welding power source can also be configured according to application requirements.
ZDH-300 Technical Specifications
| Parameter | ZDH-300 |
| Chuck Support* | 20–500 mm |
| Positioner Horizontal Load | 300 kg |
| Positioner Vertical Load | 150 kg |
| Tilting Angle | 0–90° |
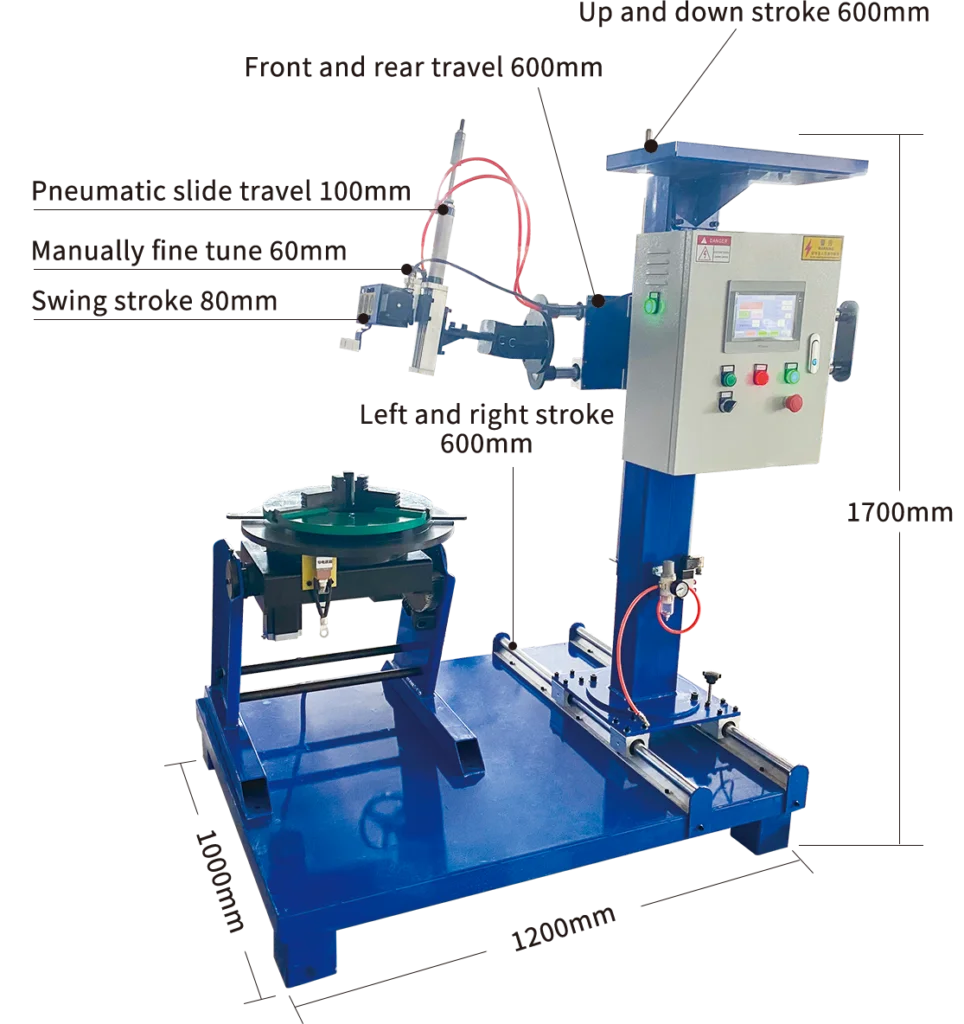
| Pneumatic Slide Travel | 100 mm |
| Manual Fine Adjustment | 60 mm |
| Oscillation Stroke | 80 mm |
| Left / Right Travel | 600 mm |
| Front / Back Travel | 600 mm |
| Up / Down Travel | 600 mm |
| Overall Dimensions | 1200 × 1000 × 1700 mm |
These specifications are based on the ZDH-300 configuration shown by the source manufacturer.
Note: Machine configuration can vary according to workpiece size, production requirements and welding process. Final specifications should be confirmed in the approved technical proposal.
Main System Components
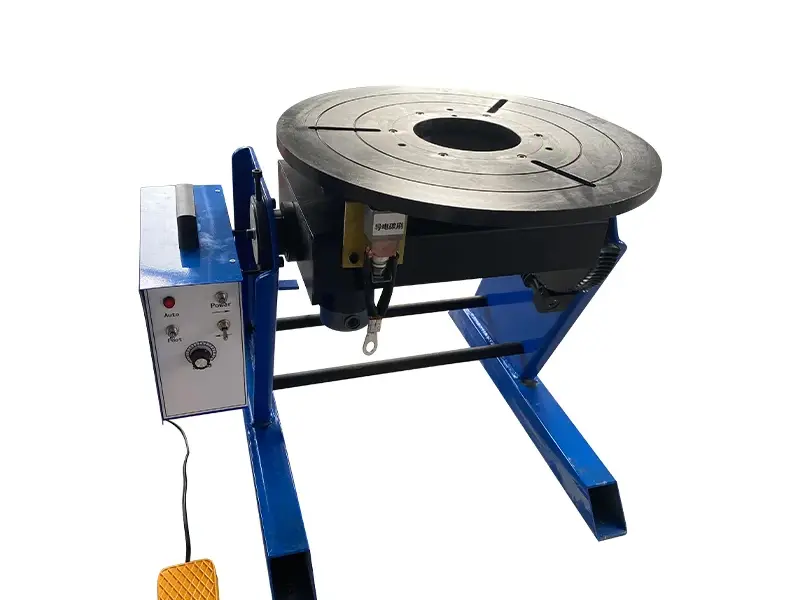
1. Welding Positioner
- The welding positioner supports and rotates the workpiece during circumferential welding.
- For the ZDH-300 configuration:
- Horizontal Load: 300 kg
Vertical Load: 150 kg
Tilting Angle: 0–90° - Controlled workpiece rotation is particularly important for obtaining stable circumferential welding conditions.
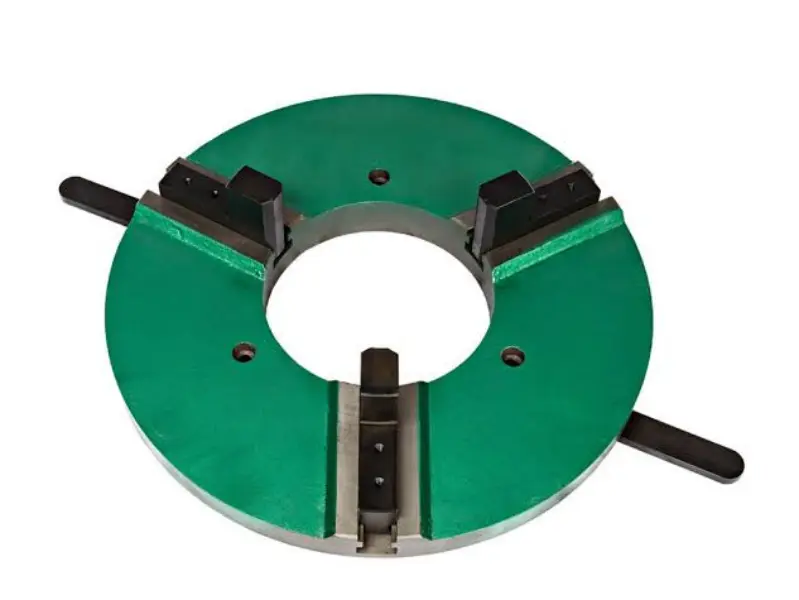
2. Workpiece Chuck
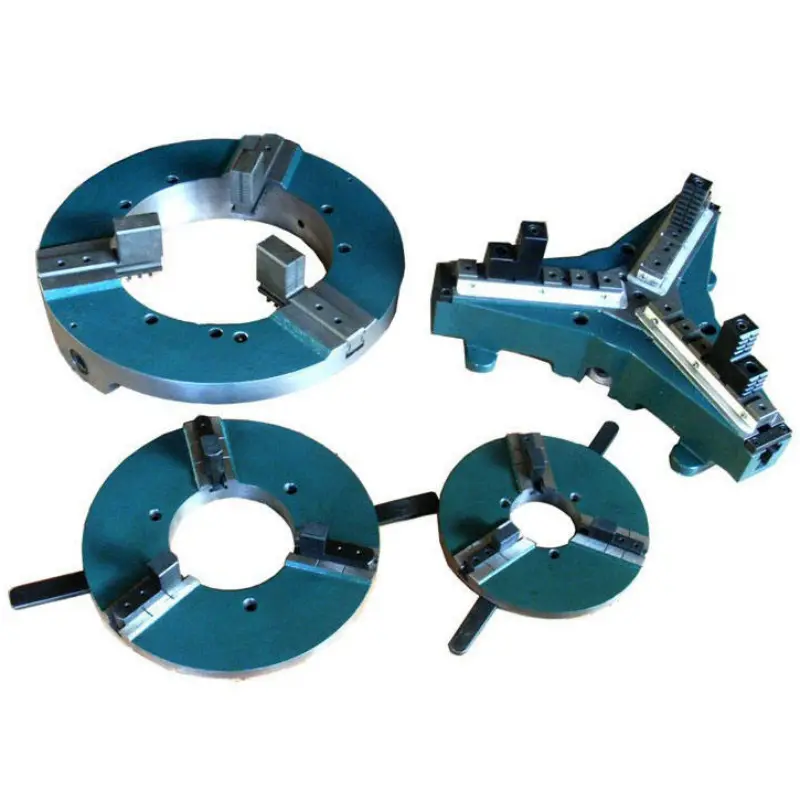
The chuck secures and centers the pipe, flange or fitting on the positioner.
WP / WPS / WPT / K11 / K12 / K13
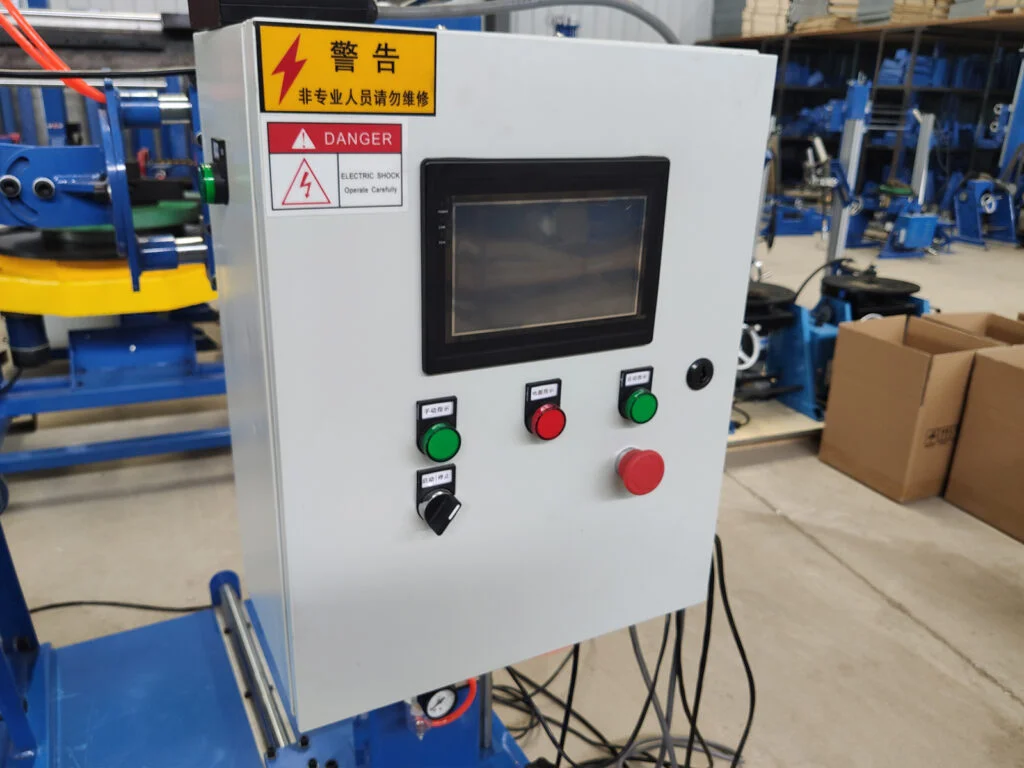
3. PLC Control System
The PLC touchscreen provides centralized control for the automated welding system and simplifies machine operation.
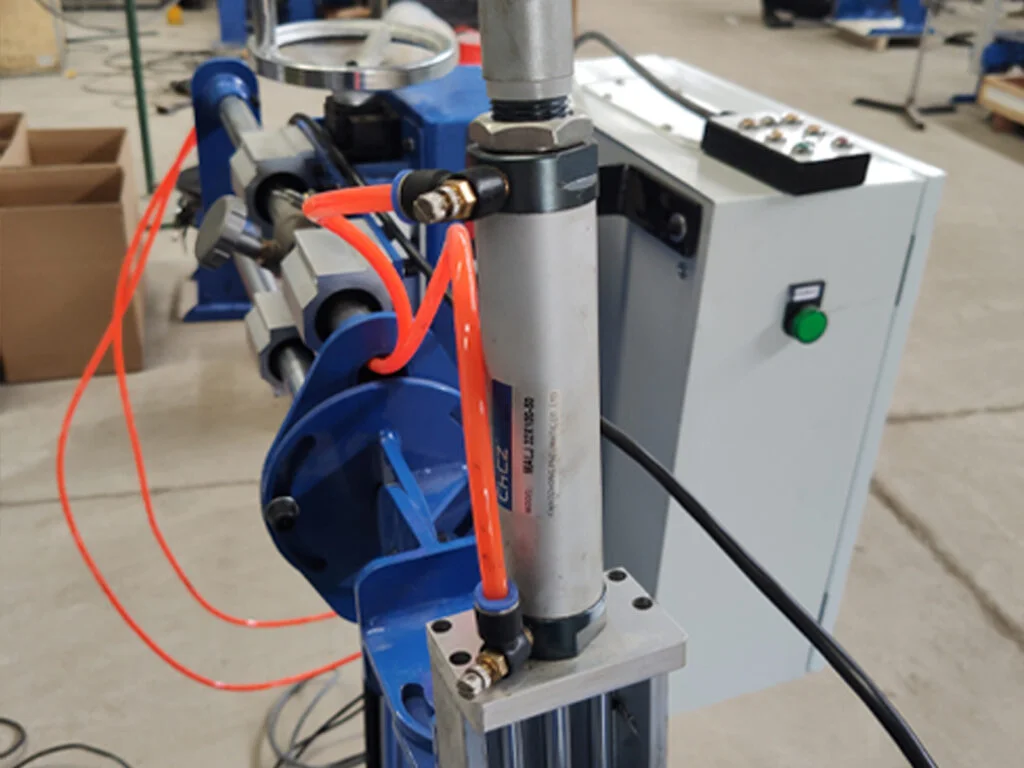
4. Pneumatic Torch Slide
A precision pneumatic slide provides 100 mm travel for torch positioning and helps facilitate workpiece loading and unloading.
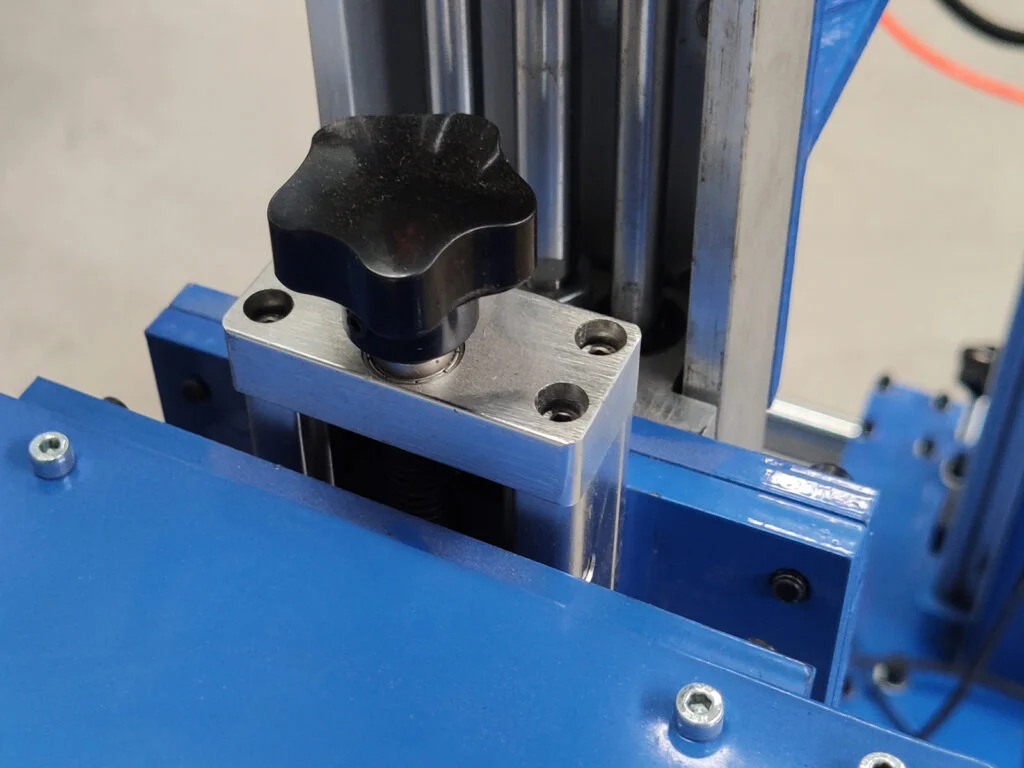
5. Manual Fine Adjustment
The system provides 60 mm manual fine adjustment for precise torch positioning.
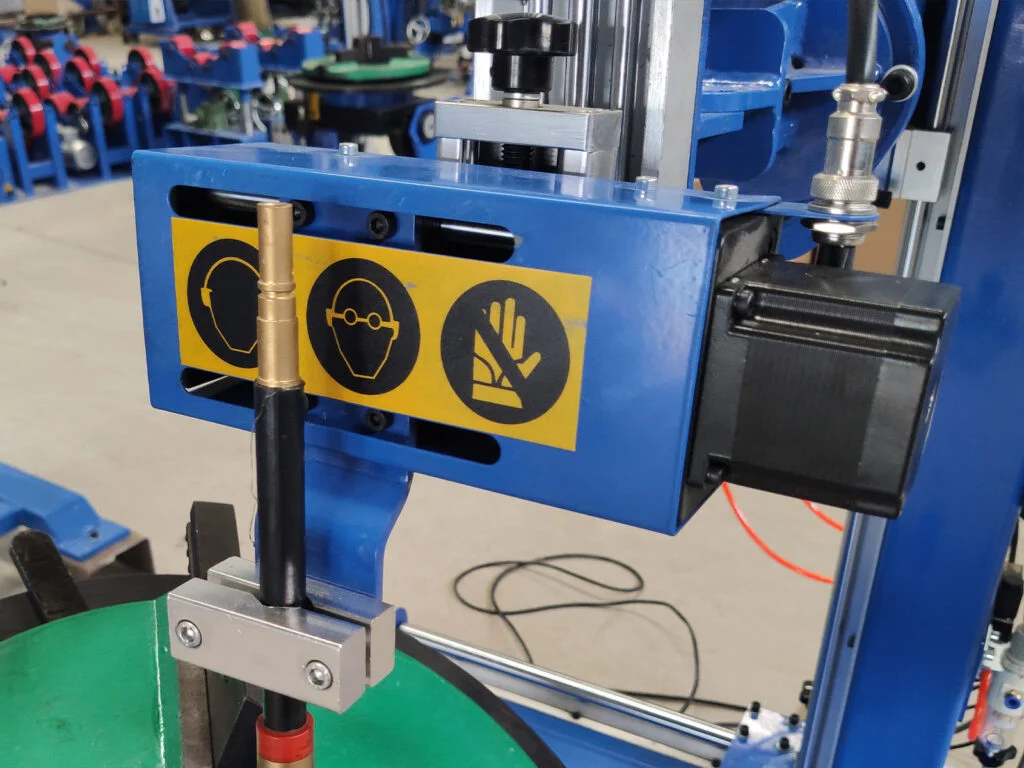
6. Welding Oscillator
The welding oscillator provides up to 80 mm stroke on the listed ZDH-300 configuration.
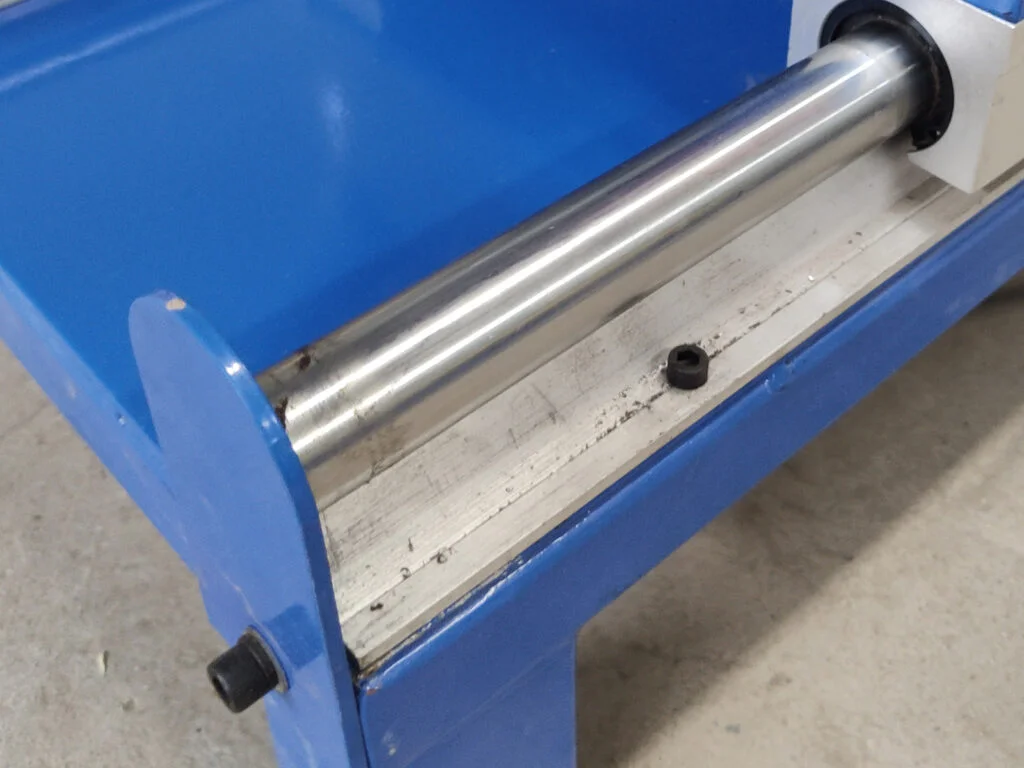
7. Precision Guide Rail
The welding unit can be repositioned along the machine structure and locked at the required welding position.
The listed machine provides 600 mm travel in left/right, front/back and up/down directions.
How the Automatic Welding System Works
01 — Load the Workpiece
Place the pipe, flange or fitting onto the welding positioner and supporting system.
02 — Clamp the Workpiece
Secure the workpiece using the chuck.
03 — Position the Welding Torch
Adjust the torch position and angle according to the weld joint.
04 — Set Welding Parameters
Set the required rotation and welding parameters according to the welding procedure and selected welding process.
05 — Start Circumferential Welding
The positioner rotates the workpiece while the welding torch performs the circumferential weld.
06 — Move to the Next Joint
For long pipe assemblies with multiple welds, reposition the welding unit for the next joint instead of repeatedly moving the entire workpiece.
Supported Welding Processes
Suitable for applications requiring gas-shielded arc welding.
Argon Arc Welding (TIG/GTAW)
CO₂ Shielded Welding
The system can be configured for CO₂-shielded welding according to production requirements.
Submerged Arc Welding
Submerged arc welding can also be configured for appropriate pipe and fabrication applications.
The source manufacturer states that the welding power source can be customized according to the required welding method.
Typical Applications
- Pipe Fabrication
Automated circumferential welding of pipe sections. - Pipe-to-Flange Welding
Suitable for flange connections requiring controlled rotational welding. - Pipe Fitting Fabrication
Applicable to elbows, tees and other pipe fittings within the machine’s configured capacity. - Long Pipe Assemblies
Particularly suitable for long assemblies containing multiple weld joints. - Fabrication Workshops
Suitable for workshops seeking to reduce manual workpiece repositioning during repetitive circumferential welding operations.
Why Use an Automatic Pipe Welding Machine?
- Consistent Workpiece Rotation
Controlled positioner rotation helps maintain stable movement during circumferential welding. - Reduced Manual Repositioning
The cantilever structure allows the welding system to move between weld locations rather than repeatedly moving long pipe assemblies. - Adjustable Torch Position
Multi-direction adjustment allows the welding torch to accommodate different workpiece dimensions and joint locations. - Flexible Welding Process Configuration
The system can be configured around different welding processes and welding power sources. - Integrated Workholding
Chuck, positioner and welding equipment work together as an integrated fabrication system.
How to Select the Right Configuration
- Workpiece Information — Pipe OD, wall thickness, length, weight, flange/fitting dimensions.
- Joint Information — Pipe-to-pipe, pipe-to-flange, pipe-to-elbow or other configuration.
- Material — Carbon steel, stainless steel or other material.
- Welding Process — Argon arc, CO₂ shielded or submerged arc welding.
- Production Requirement — Number of weld joints and expected daily production.
- Existing Welding Power Source — Specify whether the customer already has a compatible welding power source.
- Automation Requirement — Specify required torch movement, oscillation and workpiece positioning.
Automatic Welding Machine + Welding Chuck
The performance of an automatic circumferential welding system depends not only on the welding process, but also on secure workpiece clamping and controlled rotation.
MecBase can supply welding chucks for different workpiece sizes and workholding requirements, including:
WP Series — Lightweight self-centering welding chucks
WPS Series — Large through-bore welding chucks
WPT Series — Wide-range welding positioner chucks
K11 Series — 3-jaw heavy-duty chucks
K12 Series — 4-jaw heavy-duty chucks
K13 Series — 6-jaw heavy-duty chucks
Request a Quote
Need an Automatic Pipe & Flange Welding Solution?
Send us your workpiece drawings and welding requirements. We can evaluate the machine configuration according to your pipe size, workpiece weight and welding process.
| RFQ Information | Customer Input |
| Application | Pipe-to-Pipe / Pipe-to-Flange / Pipe-to-Elbow / Other |
| Pipe OD | ___ mm |
| Wall Thickness | ___ mm |
| Pipe Length | ___ mm |
| Workpiece Weight | ___ kg |
| Material | ___ |
| Flange / Fitting Size | ___ |
| Welding Process | Argon Arc / CO₂ / SAW |
| Number of Welds per Workpiece | ___ |
| Required Production | ___ pcs/day |
| Welding Power Source Required | Yes / No |
| Quantity | ___ |
Please send workpiece drawings, weld joint details and production requirements with your RFQ.
Frequently Asked Questions
It is an automated welding system that combines workpiece clamping, rotational positioning and welding equipment to perform circumferential welds on pipes, flanges and fittings.
The source machine is described for pipe-to-pipe, pipe-to-flange and pipe-to-elbow welding, as well as other pipe fittings such as tees.
The equipment can be configured for argon arc welding, CO₂-shielded welding and submerged arc welding.
The listed ZDH-300 has a 300 kg horizontal positioner load and 150 kg vertical load. Its source specification lists “Chuck support: 20–500 mm.”
Yes. The system includes manual adjustment, pneumatic slide movement and multi-directional travel for adapting the torch position to different workpieces.
Yes. The source manufacturer states that the welding power source can be configured according to application requirements.